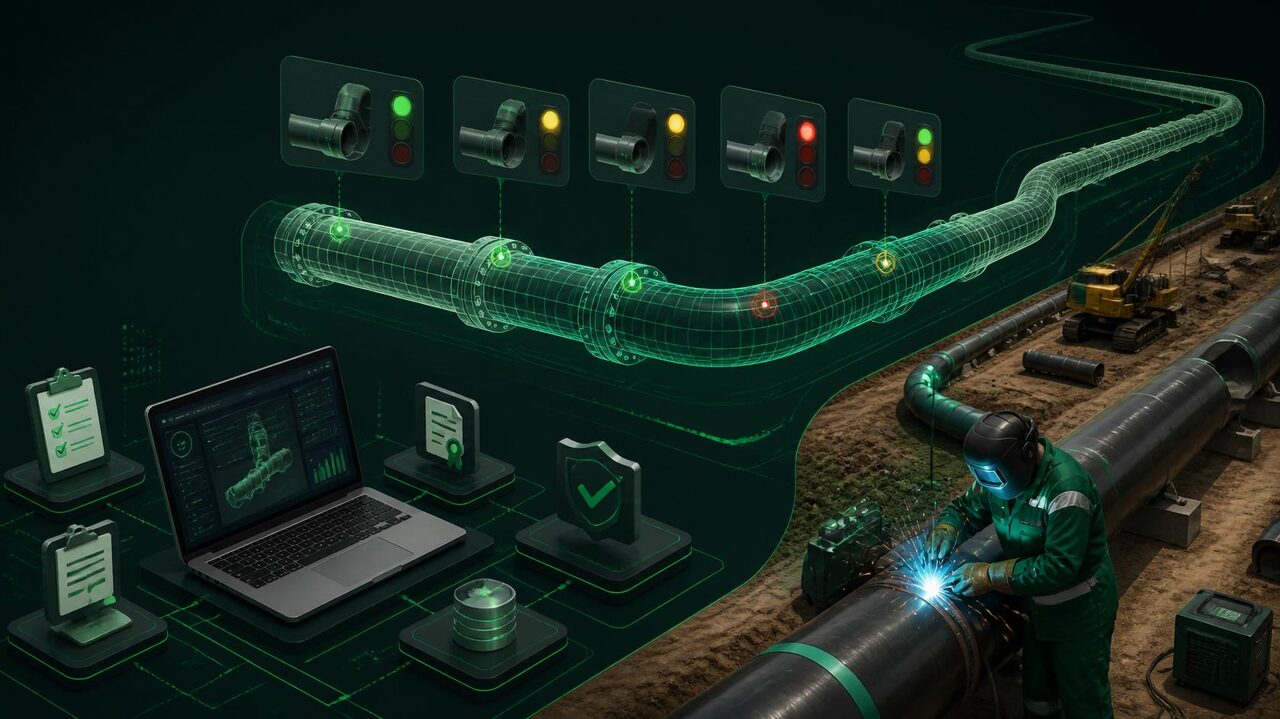
The Real Pains of Pipeline Construction
This is not theory. These are the points where the schedule melts, costs blow up, and the audit fails — and no spreadsheet solves it.
- Manual Initial Load and Human ErrorTyping thousands of joints, spools, lines and isometrics takes weeks. Every error becomes a duplicated joint, a phantom tie-in on the physical tree, and rework nobody catches until it is too late.
- Welder Outside Qualification (ASME IX)A root pass laid by a welder with an expired WPQ, outside the diameter/thickness range, or an unqualified process. Discovered at audit time — when the repair already cost a cut and refabrication.
- Uncontrolled Repair RateA welder above 2.5% keeps producing because nobody sums the linear length in real time. The index blows up, the joint reaches its 3rd defect and becomes "cut and refabricate" — a direct loss of labor-hours and material.
- Handover That Stalls CommissioningData Book stalled by a missing VT/NDT report, an open Punch List A, and Mechanical Completion that never closes. The plant is physically ready but has no dossier — while the contractual penalty clock runs.
The Real Pains of Pipeline Construction
This is not theory. These are the points where the schedule melts, costs blow up, and the audit fails — and no spreadsheet solves it.
Manual Initial Load and Human Error
Welder Outside Qualification (ASME IX)
Uncontrolled Repair Rate
Handover That Stalls Commissioning
Invalidated Hydrostatic Test
Traceability That Does Not Exist
The Definitive Solution: How PipeFlow Solves It
Materials engineering, welding planning, QA/QC and handover in a single platform — with the code embedded in the workflow, not in a PDF in a drawer.
AI Isometric Digitization
Bulk Import via Excel
Synchronous Compliance Block
Complete Physical Hierarchy
Navigable Digital Twin
Welder and WPQ Management
Shielded Pressure Tests
Handover and Data Book
From Spool to Handover — in a Single Flow
Each stage feeds the next. Data is entered once and flows through the entire quality cycle with no manual re-entry.
Engineering
Fabrication
Welding
Quality
Commissioning
PipeFlow MES vs Legacy Systems
| Feature / Capability | Spreadsheets & Legacy | PipeFlow MES |
|---|---|---|
| Weld Traceability | Manual / passive on paper | Active, tied to WPS/PQR and stamp |
| Expiration Blocking | Depends on later audit | Synchronous hard block at entry |
| Welder Repair Rate | Summed by hand, too late | Real-time mm calculation + suspension |
| Isometric Loading | Joint-by-joint typing | AI + Excel with validation and inline corrector |
| Hydrostatic Test | Gauge with no validity control | ST blocked without valid calibration |
| Handover / Commissioning | Weeks compiling scattered reports | Data Book, Punch and FMT in 1 click |
| Audit and Log | Who touched it? Nobody knows | Complete audit trail per user |
Built for Those Accountable for the Job
Each role sees exactly what it needs — and is accountable for what it logs, with a full audit trail.
Construction Coordinator
Quality Inspector
Welding Engineer
Commissioning
From Oil to Clean Energy
Refineries, petrochemical plants, pipelines, or hydrogen and renewable energy plants — any pipe assembly subject to quality and commissioning standards shares the same pains. PipeFlow MES was built for any sector that needs to trace joint by joint, control welders, and deliver a quality dossier without rework.